Overview
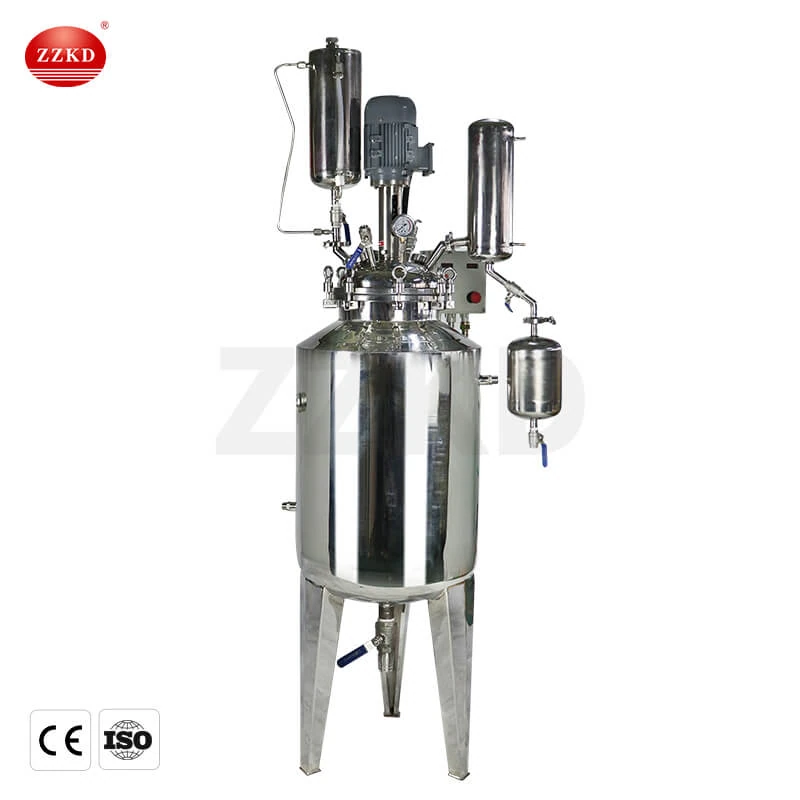
The 100L Stainless Steel Reactor is a vessel designed to carry out chemical reactions in a controlled environment. Reactors are constructed of stainless steel, a highly durable and corrosion-resistant material that can withstand harsh chemicals and high pressures.
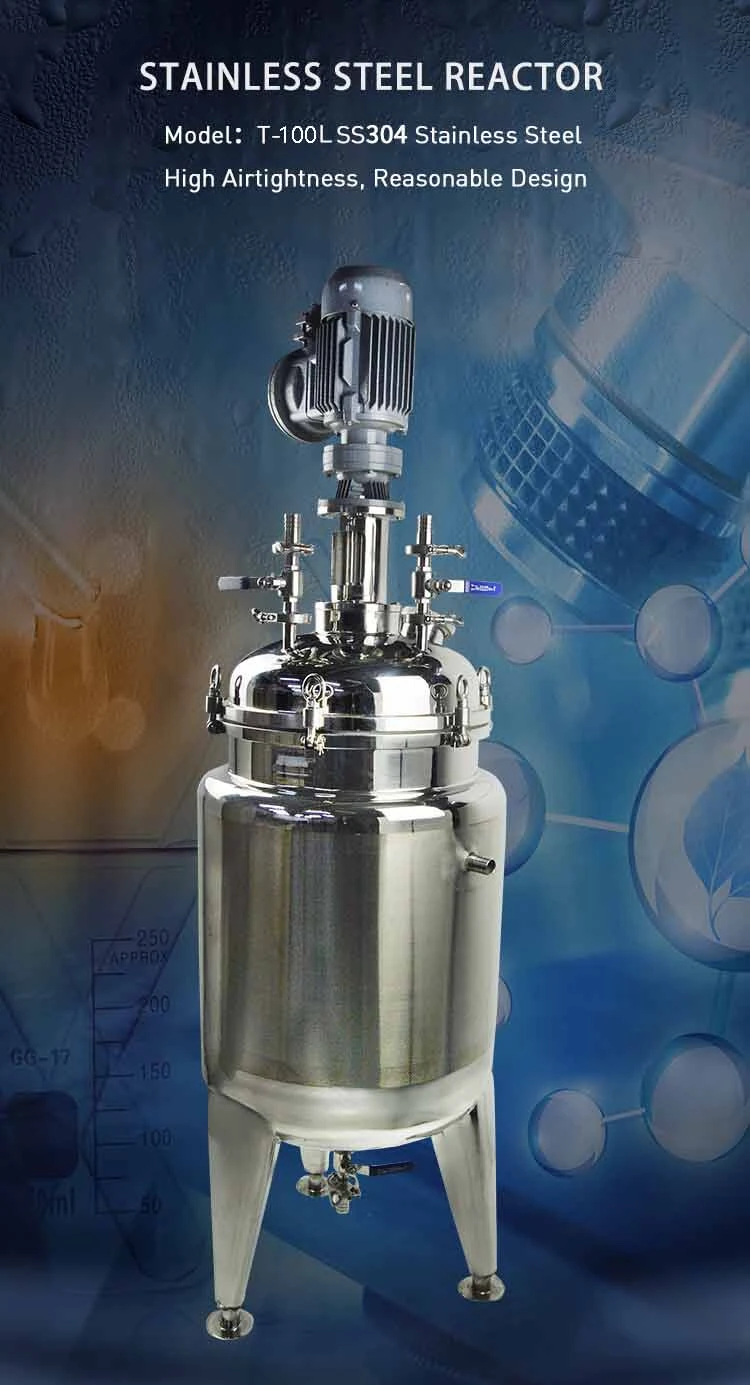
The 100 liter capacity of a reactor indicates its volume, which means it can hold up to 100 liters of reaction mixture. The size of the reactor is important because it determines the scale of chemical processes that can be performed. The 100L reactor is considered a medium-sized reactor and is often used in R&D laboratories and small-scale industrial production.
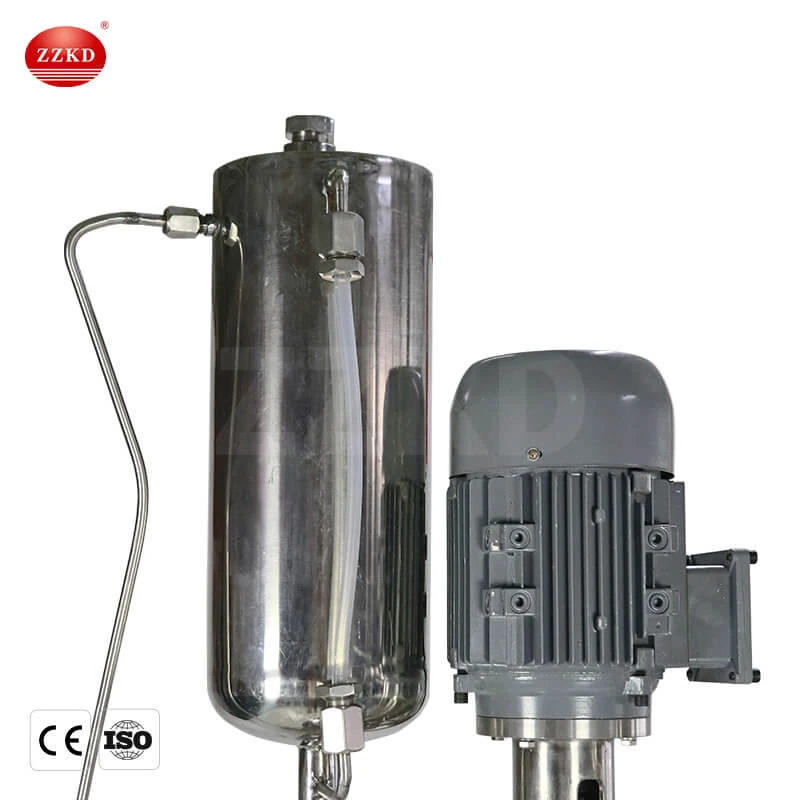
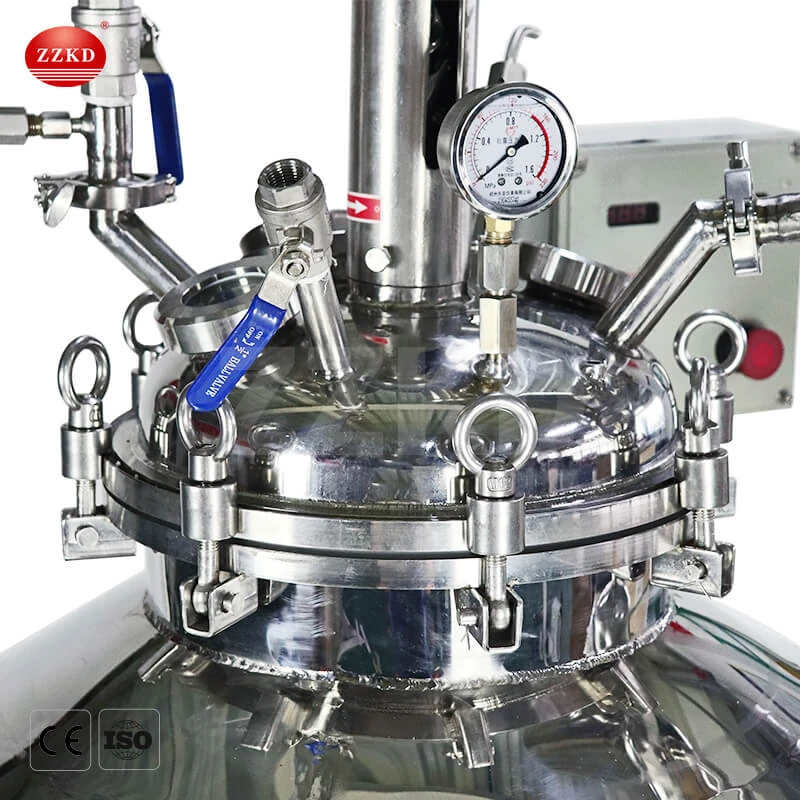
Stainless steel reactors are commonly used in the chemical, pharmaceutical and food industries, among others. They are designed with various features such as heating and cooling systems, stirring mechanisms, pressure and temperature sensors, and feeding and sampling ports.
Advantages of 100L stainless steel reactor:
1. Durability: Stainless steel reactors are extremely durable and can withstand harsh chemicals and high pressure. This makes them a reliable and long-lasting choice for chemical processing.
2. Corrosion resistance: Stainless steel has a strong ability to resist corrosion, which makes it ideal for chemical processing applications that use acidic or corrosive materials.
3. Sanitation: Stainless steel is easy to clean and maintain, which makes it a hygienic choice for industries such as food processing and pharmaceuticals.
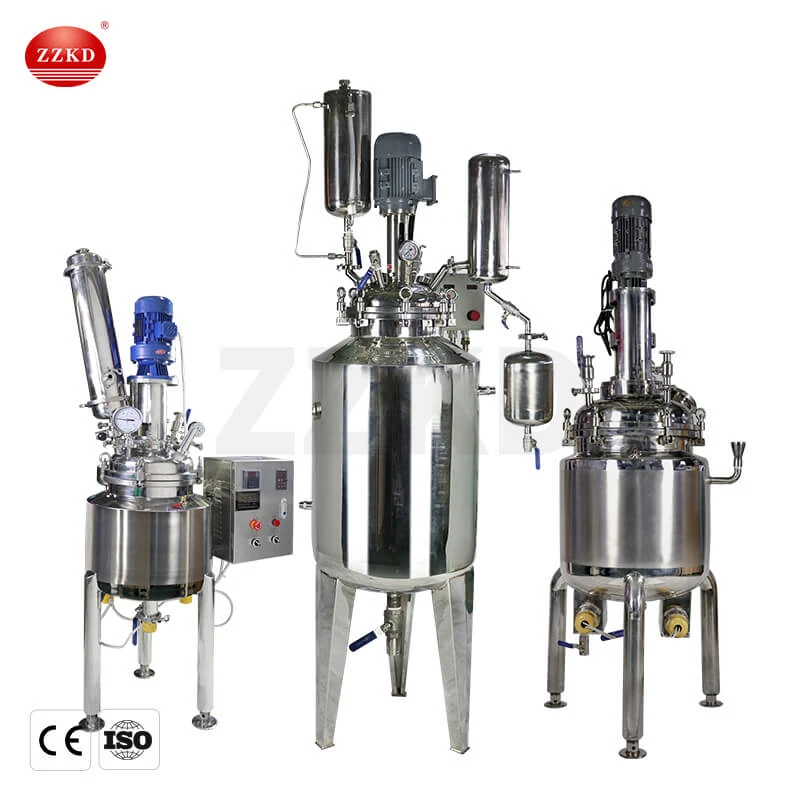
4. Customizable: 100L stainless steel reactor can be customized to meet specific process requirements. This includes features such as heating and cooling systems, stirring mechanisms, pressure and temperature sensors, and feed and sampling ports.
5. Cost-effective: Stainless steel reactors are a cost-effective option for conducting chemical reactions because they have a long service life and require minimal maintenance.
6. Versatility: Stainless steel reactors can be used in a wide range of chemical processes, making them a versatile choice for R&D laboratories and small-scale industrial production.
The advantages of the 100L Stainless Steel Reactor make it a popular and reliable choice for chemical processing applications.
Features
100L stainless steel reactor application:
100L stainless steel reactor can be widely used in chemical, pharmaceutical, food and other industries.
1. Chemical synthesis: 100L stainless steel reaction kettle can be used for chemical synthesis such as polymerization, esterification and hydrolysis.
2. Process development: The reactor can be used to develop new chemical processes and formulations.
3. Drug development: 100L stainless steel reaction kettle can be used for the development of new drugs and drug dosage forms.
4. Food processing: The reactor can be used for food processing, such as fermentation, stirring, emulsification, etc.
5. Petrochemical industry: The reactor can be used in cracking, polymerization, hydrogenation and other processes in the petrochemical industry.
6. Environmental remediation: The reactor can be used in the treatment of industrial waste and wastewater, such as bioremediation, oxidation and reduction processes.
7. Specialty chemicals: 100L stainless steel reactor can be used to produce specialty chemicals, such as surfactants, adhesives, coatings, etc.
The versatility of the 100L stainless steel reactor makes it an invaluable tool in areas such as the chemical, pharmaceutical and food industries.
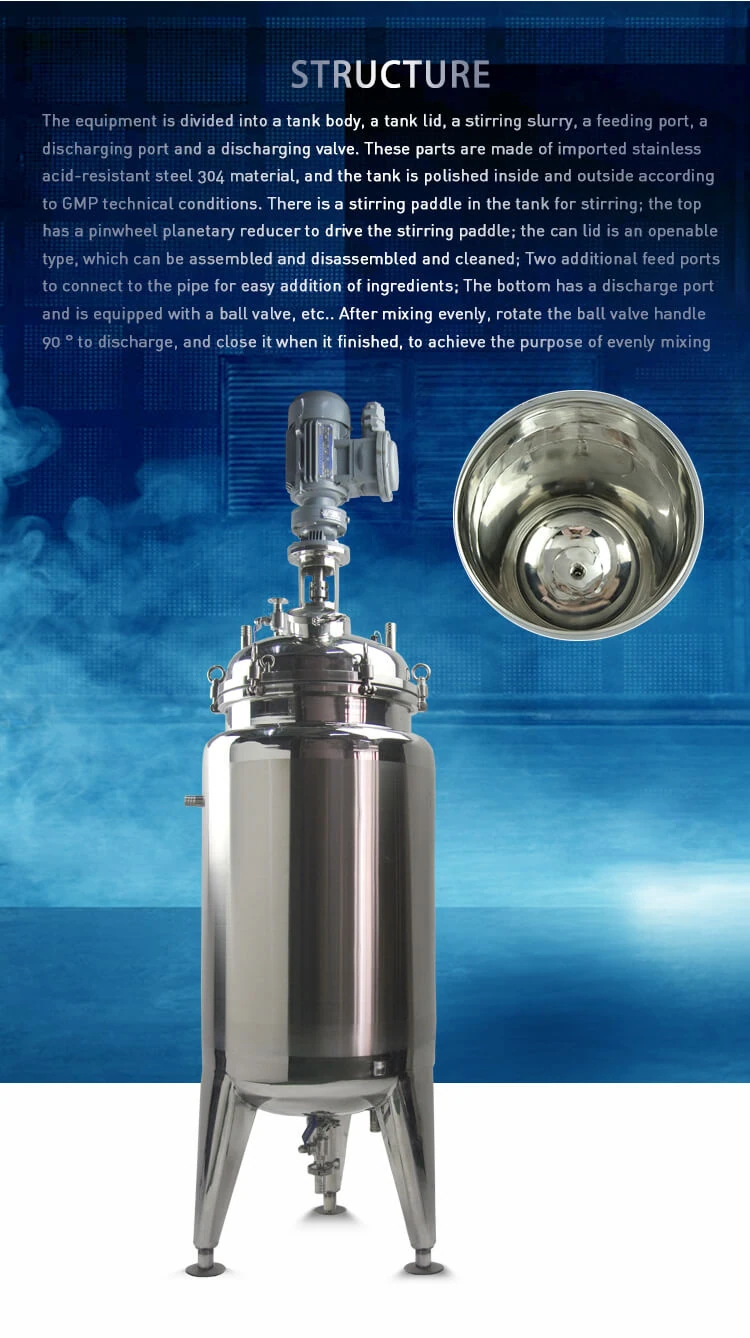
100L stainless steel reactor operation method:
The operation of the 100L stainless steel reactor depends on the specific process requirements, but generally includes the following steps:
1. Preparation: Before starting the process, the reactor should be thoroughly cleaned and any required accessories installed, such as stirrers and sensors. Reactants should be prepared according to process requirements.
2. Loading: The reactants are loaded into the reactor through the appropriate ports, which are usually located at the top of the vessel. The reactor should be filled to an appropriate level, taking into account any expansion that may occur during the reaction.
3. Heating or Cooling: The reactor may need to be heated or cooled to maintain the temperature required for the reaction. This can be achieved using an external heating or cooling system connected to the reactor through appropriate ports.
4. Mixing: Use a stirrer or stirrer installed inside the reactor to mix the reactants. The speed and direction of the stirrer should be adjusted to ensure proper mixing of the reactants.
5. Reaction monitoring: Use sensors installed in the reactor to monitor temperature, pressure and other relevant parameters throughout the reaction process. Make any necessary adjustments to maintain desired reaction conditions.
6. Sampling: Samples are taken from the reactor at various stages of the process to monitor the progress of the reaction and ensure that the product meets the required specifications.
7. Discharge: After the reaction is complete, the product is discharged from the reactor through an appropriate port, usually located at the bottom of the vessel.
8. Cleaning: The reactor should be cleaned thoroughly after each use to prevent contamination and ensure readiness for the next process.
The operation of the 100L stainless steel reactor requires careful attention to process parameters to ensure a successful and safe reaction.
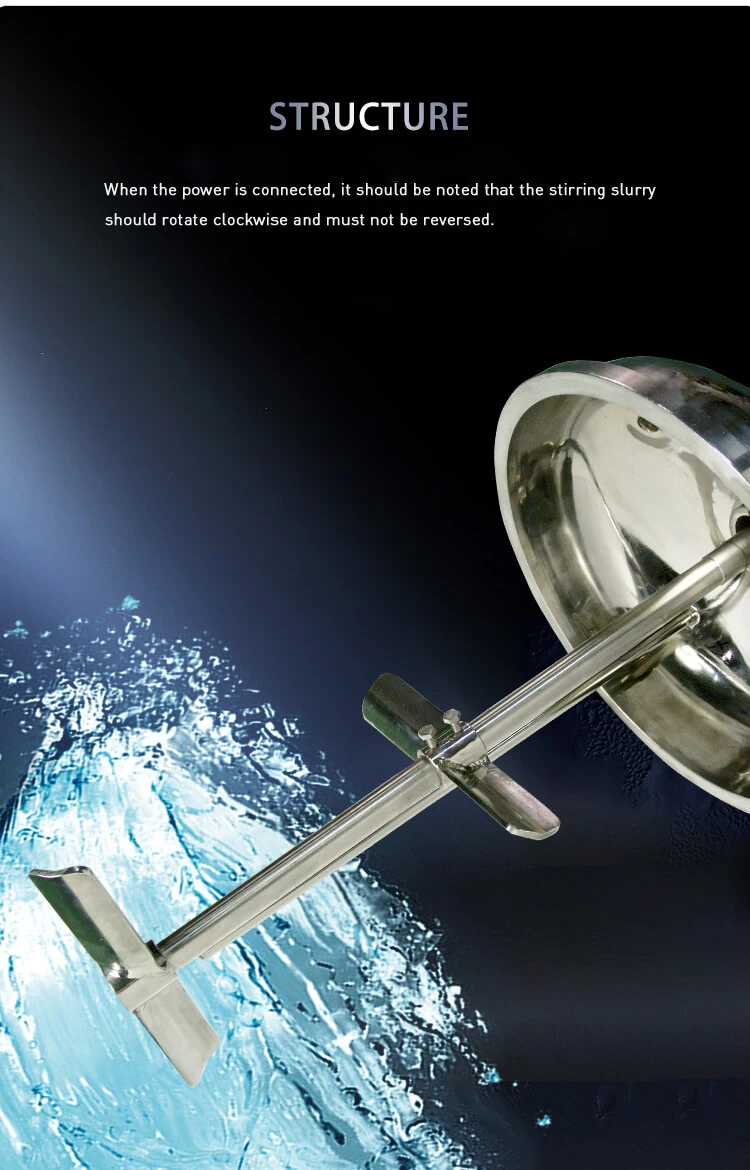
Specifications
|
Model |
SS-100L |
|
Capacity |
100L |
|
Jacket capacity |
30L |
|
Voltage |
220V/50HZ |
|
Working pressure |
Ordinary pressure |
|
temperature |
0-250℃ |
|
Power |
400W |
|
Frequency |
0-500 r/min |
|
Maximum torque |
273 N/CM |
|
Heating mode |
Sandwich oil bath |
|
Material |
304/316 |
|
Sealing mode |
Mechanical seal |
FAQ:
1. What material is the 100L stainless steel reactor made of?
The 100L stainless steel reactor is made of high-quality stainless steel, which is resistant to corrosion, wear and high temperature. Specific grades of stainless steel may vary depending on process requirements.
2. What is the maximum working temperature of the 100L stainless steel reactor?
The maximum working temperature of the 100L stainless steel reactor depends on the specific grade of stainless steel used and the design of the reactor. Typically, stainless steel reactors can operate at temperatures up to 400°C.
3. Can the 100L stainless steel reactor be used for dangerous goods?
Yes, 100L stainless steel reactors can be used for hazardous materials provided the reactor is designed to handle the specific hazard and safety measures are in place.